KDR Automation

Obsolete PLC? Keep the machine. Replace the controls.

When the controller is end of life, spares are scarce and the original builder has gone, one fault can stop a line for weeks. We back up what is there, work out what it actually does, and rebuild it on current hardware, tested off site so your shutdown is short.

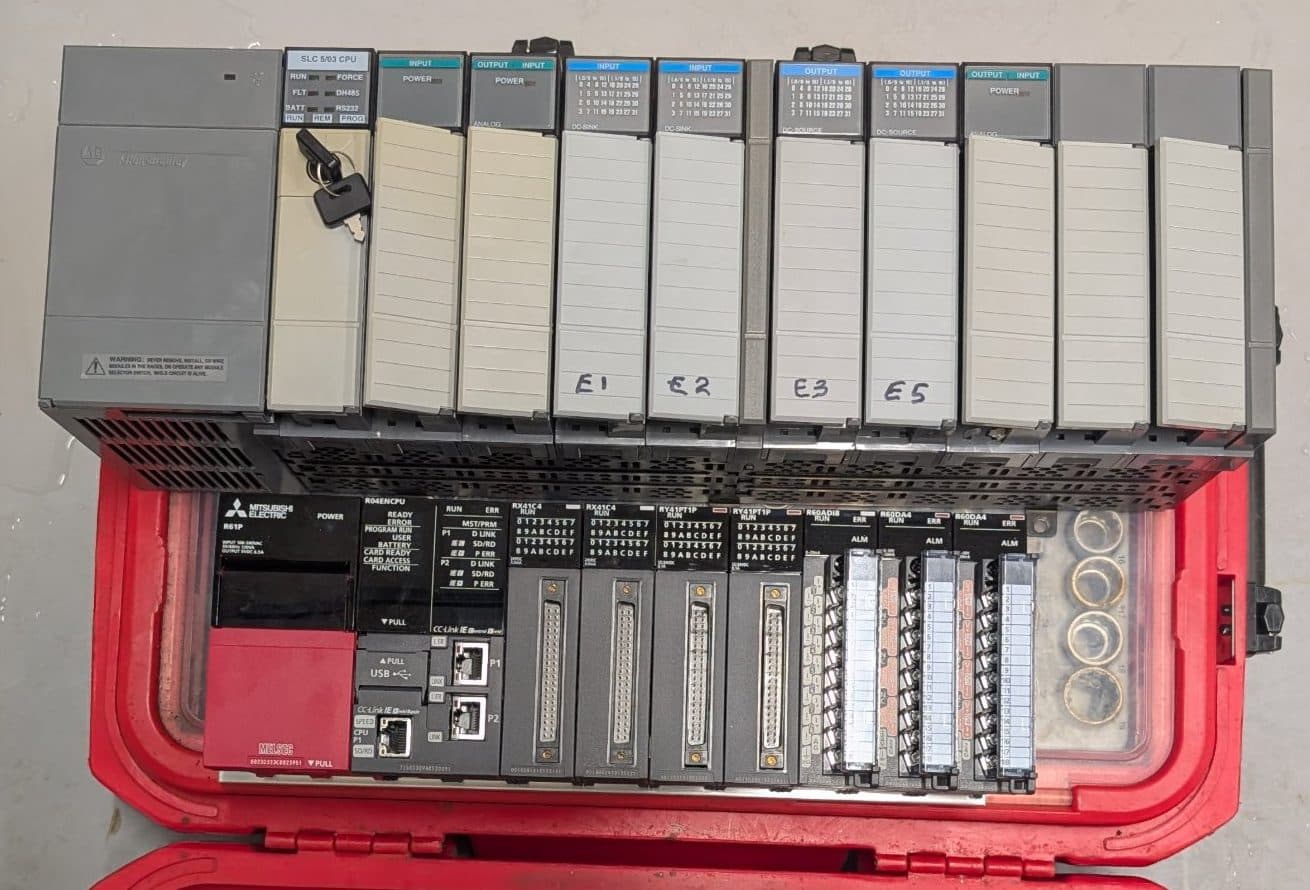
An Allen Bradley SLC 5/03 rack sitting above the Mitsubishi iQ-R rack that replaced it

Signs it is time

  • Spare parts are only available second-hand, if at all
  • The program has never been backed up, or nobody knows where the backup is
  • The programming software only runs on one old laptop
  • The original machine builder or integrator no longer exists
  • The HMI is failing, or the screens are hard to read
  • Breakdowns take longer to fix because nobody understands the code

What we upgrade from

  • Allen Bradley SLC 500 and PLC-5
  • Siemens S5 and S7-300
  • Mitsubishi A and Q series
  • ifm controllers
  • Red Lion and other legacy HMIs
  • Other platforms: ask us

How we do it

  1. 01Backup and surveyBack up the existing PLC and HMI, record the I/O and watch the machine running.
  2. 02Reverse engineerWork through the program and write down what the machine actually does, so nothing is lost.
  3. 03Agree the scopeLike-for-like, or with improvements such as clearer alarms and diagnostics.
  4. 04Build and test off siteNew code and hardware tested in our workshop before your shutdown.
  5. 05CutoverWhere it helps, we make up conversion cables so the new PLC plugs into the existing wiring. Then we check every I/O point and run the SAT with your operators.

What you are left with

  • A supported PLC and HMI, with spares available
  • A clean, commented program that you own
  • Updated drawings and a backup of the final code
  • Better alarm and fault screens than before

Related projects

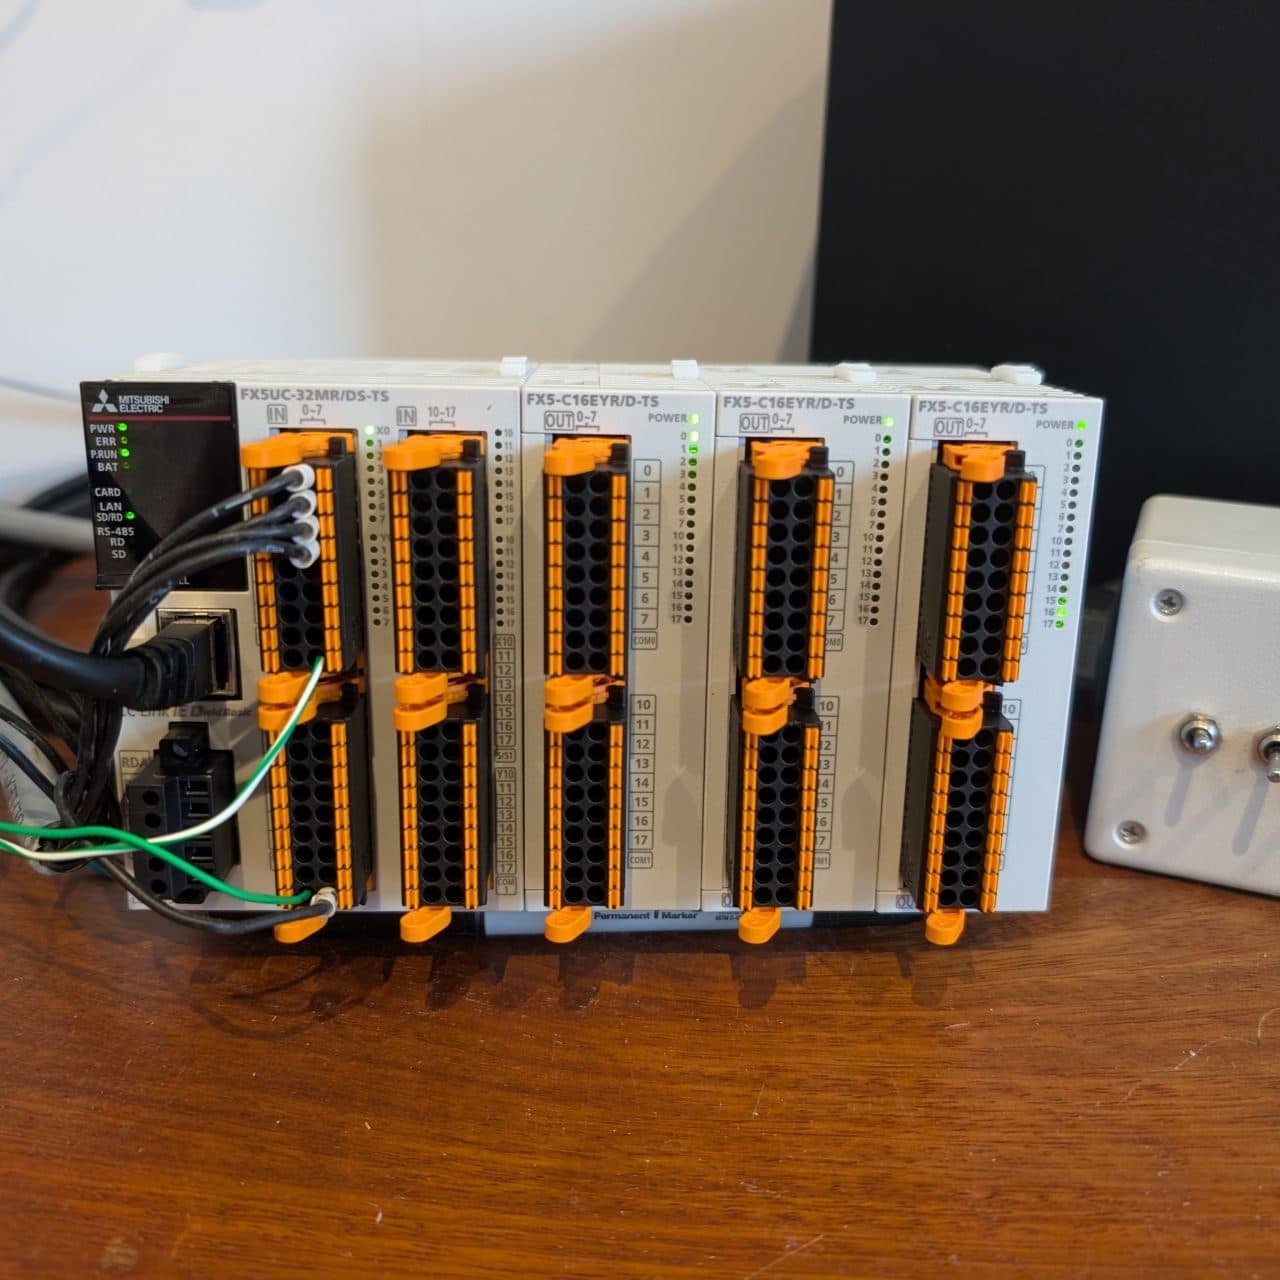
Mitsubishi FX5UC PLC with three 16-point output modules and orange spring clamp connectors, wired up for bench testing

Asphalt productionUpgrade

Asphalt plant filter valve control upgrade

A failed, obsolete control board on an asphalt plant's filter replaced with a Mitsubishi FX5UC PLC, now controlling 48 valves across multiple cleaning sequences.

Old control
Failed obsolete control board
New PLC
Mitsubishi iQ-F FX5UC
I/O
16 inputs, 64 outputs
The original Allen Bradley SLC 5/03 rack sitting above the Mitsubishi iQ-R rack that replaced it

Meat processingUpgrade

Spiral blast freezer control upgrade

An obsolete SLC 5/03 and Red Lion HMI replaced with Mitsubishi iQ-R and GOT2000 after the original builder closed, with the program reverse engineered from a backup.

Old PLC
Allen Bradley SLC 5/03
New PLC
Mitsubishi iQ-R R04EN
HMI
Red Lion to GOT GT2510
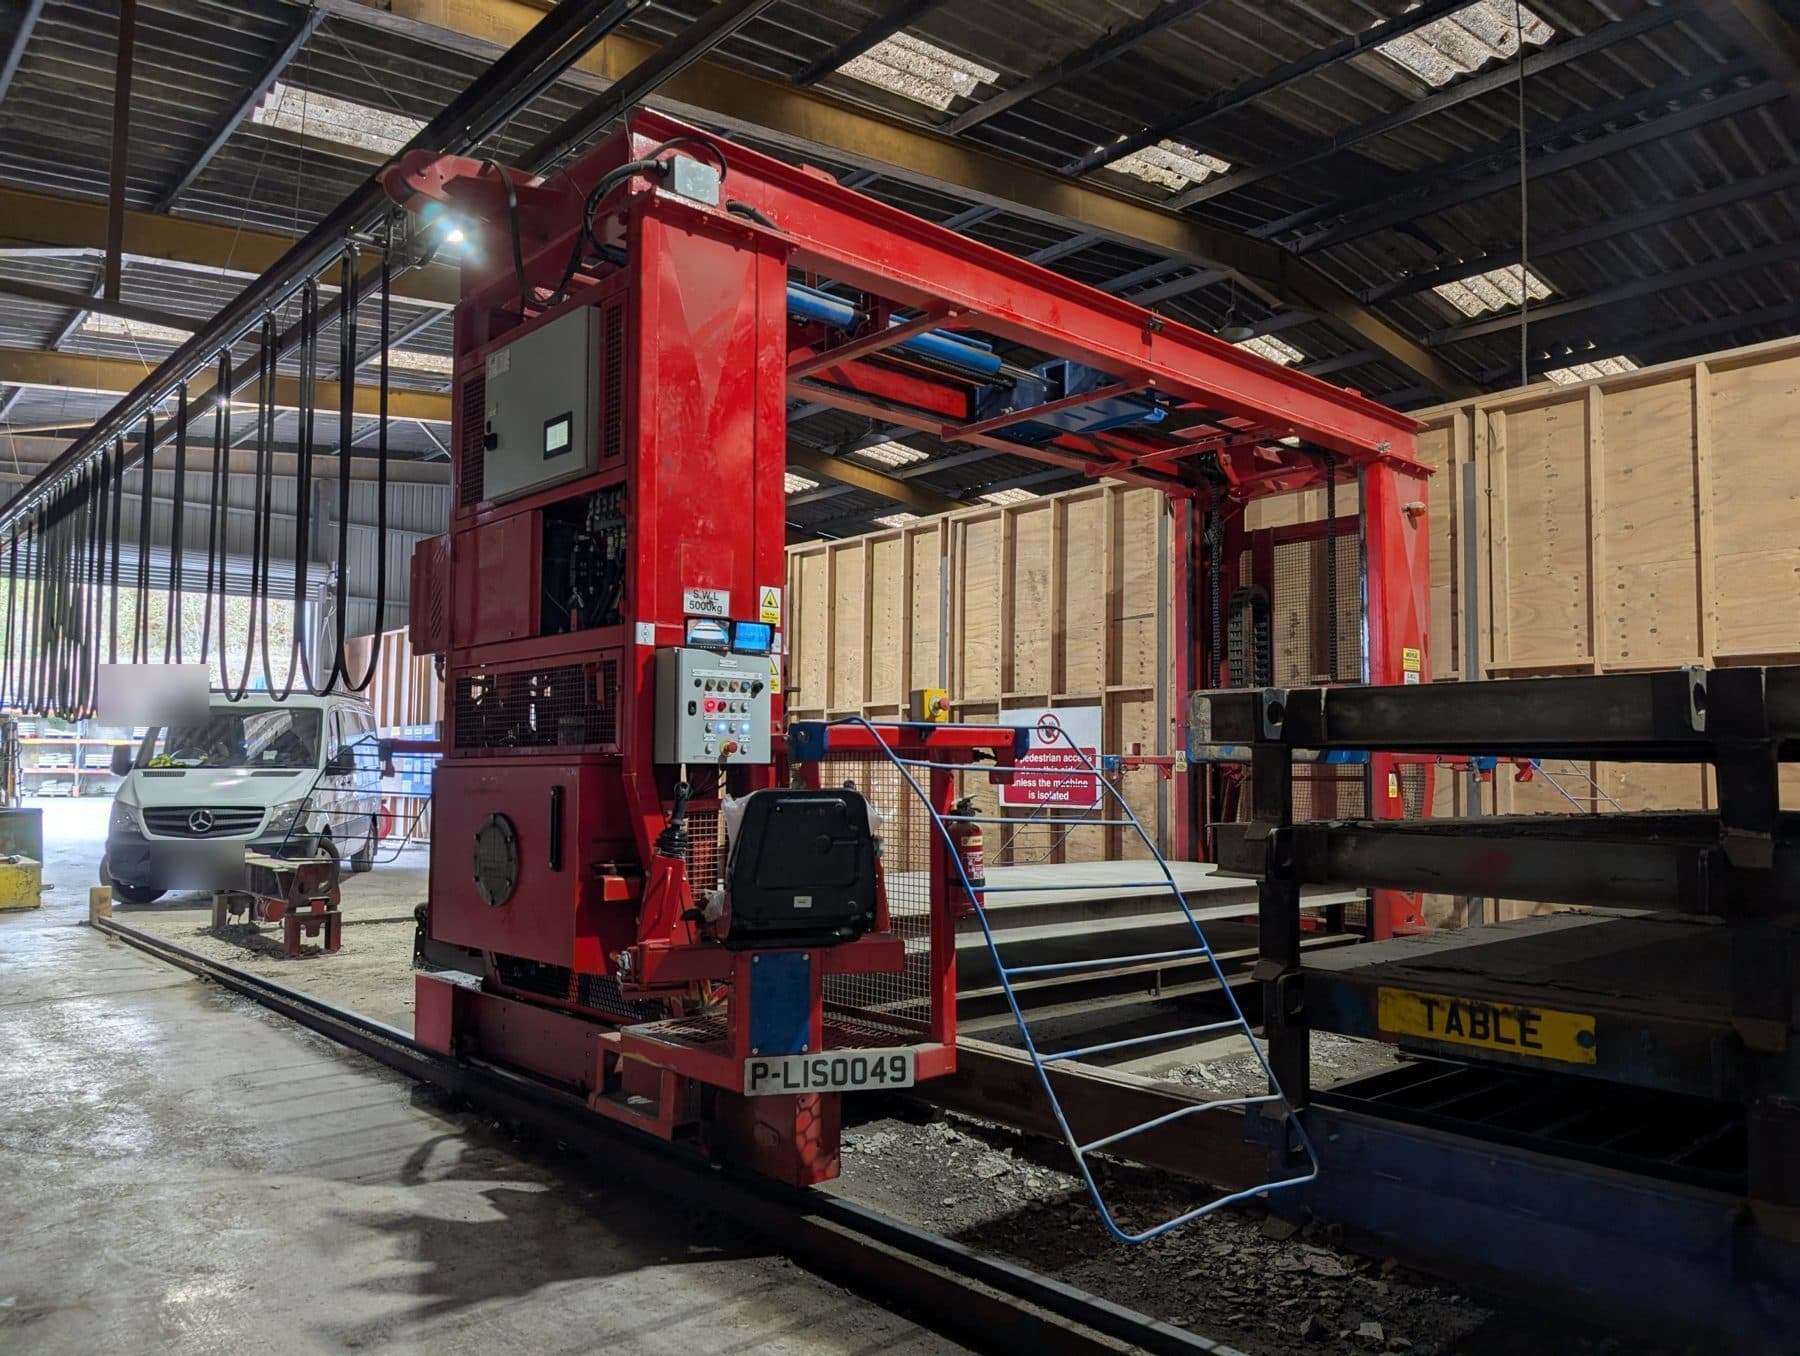
Red rail-mounted precast concrete handling machine in a production shed

Precast concreteUpgrade

Precast handler control upgrade in a single day

Ageing Allen Bradley controls on a rail-mounted precast handler replaced with a Mitsubishi FX5UC, a new operator HMI and Weidmüller remote IO, installed and SAT tested in one day.

PLC
Allen Bradley to Mitsubishi FX5UC
Remote IO
Weidmüller UR20, Modbus TCP
On site
1 day, including SAT

Further reading

Common questions

How long will the machine be down?

It depends on the size of the machine, but because the new system is built and tested before we arrive, the on-site work is mostly installation and testing. On a recent handler upgrade the machine was back in production the same day, including the SAT.

We do not have the original program. Can you still help?

In most cases we can upload the program directly from the running PLC. Comments and tag names are often missing, which is why we reverse engineer and document the logic before rewriting it.

Will the machine work the same afterwards?

That is the default. Operators keep the sequences and settings they rely on, unless we have agreed improvements with you.

Can we keep the existing wiring?

Usually the field wiring and devices stay. New I/O is mapped to the existing terminals, and on rack-based PLCs we often make up conversion cables in advance so the new PLC connects to the existing wiring. That keeps the cutover quick and the risk low.

Which platform will you move us to?

Normally your site standard. Recent upgrades have moved Allen Bradley and ifm systems to Mitsubishi FX5 and iQ-R, and we also work in Siemens and current Allen Bradley platforms.

Project enquiry

Got a machine that worries you?

A few details and a photo of the panel are enough to start. You will hear back directly from an engineer.

We use your details only to reply. See our privacy policy.